 Request a Quote
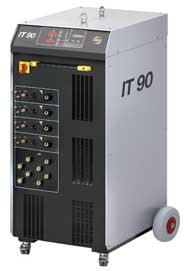
Inverter Arc Stud Welder - IT 90 AT
The IT 90 AT is a high-current inverter arc stud welder delivering up to 2,000 A for large-diameter stud welding. It supports ARC and Short Cycle welding, studs from M3 to M24, and automated configurations with optional four-gun/head connections.
GENERAL INFORMATION
Application
- Especially suitable for thicker sheets of about 2 mm or higher
Equipment
- Inverter (2000 A) with options for 4 outputs, process monitoring and shielding gas
- Welding with ceramic ferrule
Technology
- 2,000 A output for heavy-duty stud welding
- M3–M24 range for large studs
- 30 kHz frequency for dynamic control
- Up to 4 heads for automation
- Process monitoring for weld consistency
- Parameter library for fast setup
- Automatic lift test for gun verification
- RS-232 interface for data transfer
Mild steel
Stainless steel
Aluminium
M3 to M24 - #4 to 1"
| FEATURES |
|---|
|
| Advantages |
|---|
Structure
|
Safety
|
Welding
|
| Technical Data | |
|---|---|
| Welding Process | ARC, SC |
| Welding material | Mild steel, stainless steel, aluminum |
| Technology | Inverter |
| Equipment | Welding with ceramic ferrule Welding with shielding gas Process control Automation 4 gun/head connections - (optional) |
| Display | Digital |
| Welding range | M3 to M24, dia. 2 to 22 mm / #4 to 1", dia. 14 ga to 7/8" |
| Welding rate | Dia. 22 / 7/8" = 6 studs/min |
| Welding current | 2,000 A (max.) |
| Current adjustment range | 300 to 2,000 A (stepless) |
| Welding time | 5 to 1500 ms (stepless) |
| Primary power | 400 V*, 3 phase, 50/60 Hz, 63 AT (slow blow) * alternative primary power available - see - Order Number below |
| Primary plug | 63 A (with 400 V mains) |
| Connected load | 100 KVA (with 400 V mains) |
| Cooling type | F (temperature controlled cooling fan) |
| IP code | IP 21 |
| Dimensions - LxWxH (without handle) | 650 x 560 x 1290 mm / 25.6" x 22" x 50.8" |
| Weight | 145 kg / 319.67 lbs (1 gun conn.) 165 kg / 363.76 lbs (4 gun conn.) |
| Suitable guns | See below |
| Order number | 93-60-12096 (400 V - 1 gun connection) 93-60-42096 (400 V - 4 gun connection) 93-66-12096 (480/460 V - 1 gun connection) 93-66-42096 (480/460 V - 4 gun connection) 93-40-019 (Ground cable, 2 pcs., 5 m, 70 mm 2, 1 vice grip 10") |
Where the IT 90 AT Fits
| Application | Why the IT 90 AT Fits |
|---|---|
| Heavy Equipment | High-current welding for large structural studs. |
| Structural Steel | Supports large-diameter studs for heavy steel assemblies. |
| Construction Equipment | Suitable for frames, chassis, and structural components. |
| Shipbuilding | High-current ARC welding for demanding steel applications. |
| Rail & Transportation | Automated stud attachment on large metal assemblies. |
| Industrial Machinery | Supports repetitive stud welding on heavy components. |
| Large Sheet Fabrication | Suitable for thicker steel sections and large studs. |
| Automated Production Lines | Up to 4 welding heads support multi-position production. |
| Pressure & Energy Equipment | High-current capacity for demanding industrial components. |
| General Heavy Fabrication | M3–M24 range covers diverse stud sizes and applications. |
FAQs
The IT 90 AT supports studs from M3 to M24 / #4 to 1 inch, with the listed welding diameter extending to 22 mm / 7/8 inch. Actual capability depends on stud type, material, and welding configuration.
A 2,000 A output provides the high welding current required for larger-diameter studs and demanding arc welding applications. The IT 90 AT is therefore suited to heavy fabrication where lower-current stud welders may not provide sufficient capacity.
Yes. The IT 90 AT is available with an optional four-gun/head connection, allowing multiple welding heads to be integrated into automated or production-oriented configurations.
Process monitoring records factors affecting each weld and compares reference values with actual values. The system can display welding energy and automatically stop welding when programmed process limits are exceeded.
Its library function can automatically specify welding current and time based on the selected stud diameter. Operators can then fine-tune the parameters using the machine controls.
The IT 90 AT uses a 30 kHz switching frequency for highly dynamic regulation of the welding process. This supports precise control of welding behavior, particularly across changing current and time requirements.
Yes. The IT 90 AT includes an automation configuration and can be equipped with automatic welding heads, including the KAH 412 and KAH 412 LA, or automatic feeding configurations using the PAH-1 and VBZ-3.
Stud Welding Guns

PAH-1 (Tripod)
M3 to M8
- Studs length (from 0.31 to 1.18") - other lengths only by request
- Universal design for flat surfaces
- Hand gun for fully automatic stud feed (with VBZ-3) or hand feed
- Recommended for large-scale production

PAH-1 (centering device dia. 30 mm)
M3 to M8
- Studs length (from 0.31 to 1.18 inches) - other lengths only by request
- Used for welding with templates
- Hand gun for fully automatic stud feed (with VBZ-3) or hand feed
- Recommended for large-scale production

KAH 412 - Automatic Stud Welding Head
M3 to M8 (dia. 10 to 12.7 mm)
- Studs length (from 0.31 to 1.18") - other lengths only by request
- Setting the lift and plunge via digital display (selection mm/inch)
- No length compensation

KAH 412 LA - Automatic Stud Welding Head
M3 to M8 (dia. 10 to 12.7 mm)
- Studs length (from 0.31 to 1.18") - other lengths only by request
- Setting the lift via adjustment screw (increments 0.1 mm)
- Length compensation of length variances in studs height and variances of the workpiece